About Industral Bleached Cotton
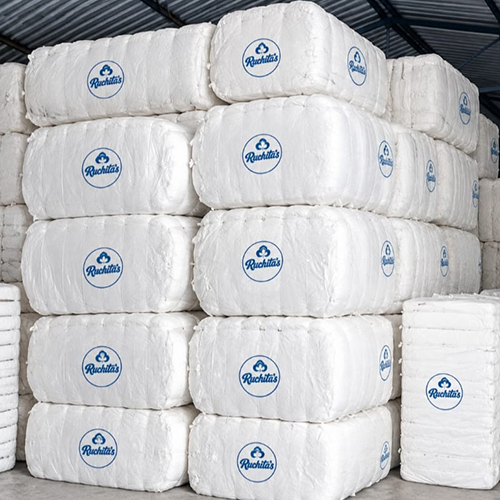
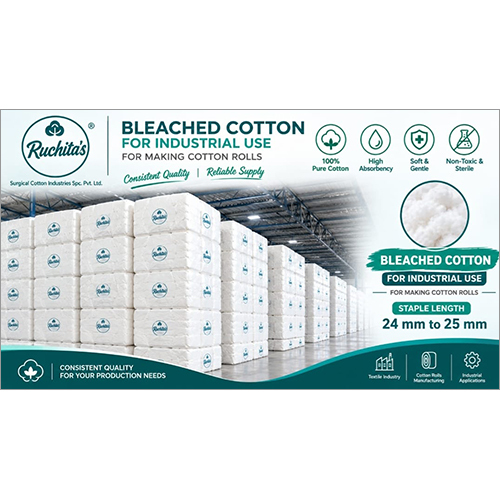
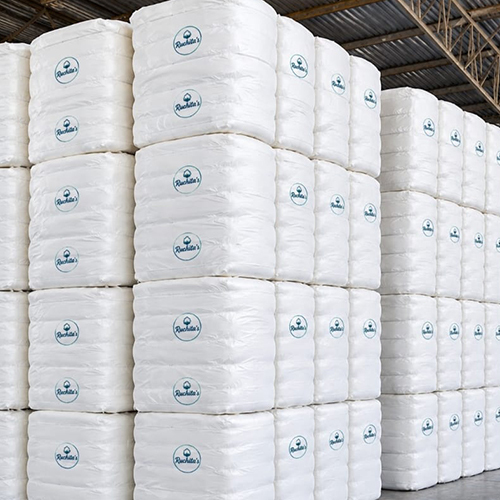
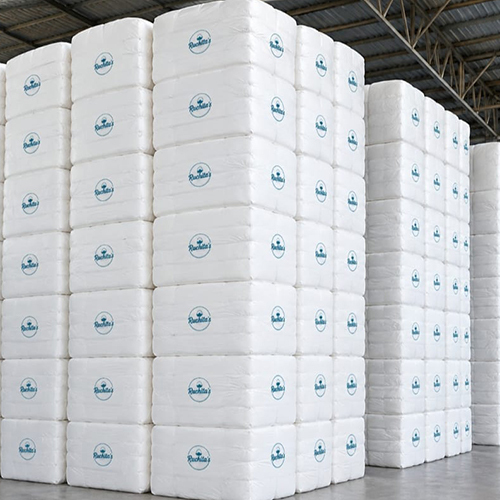
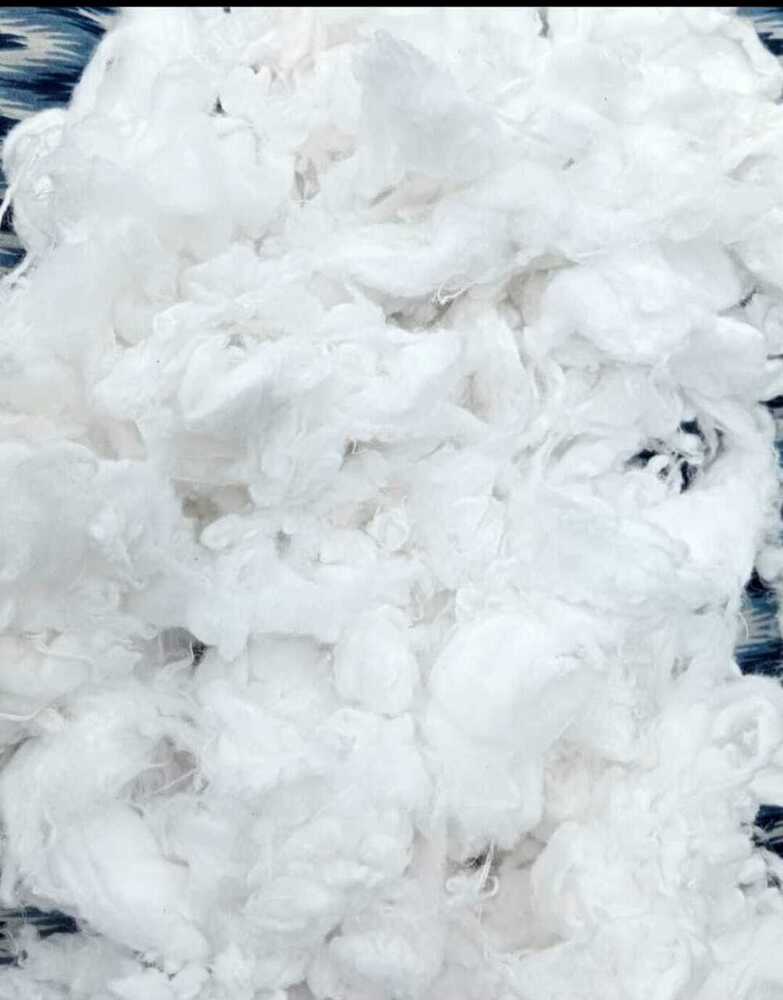
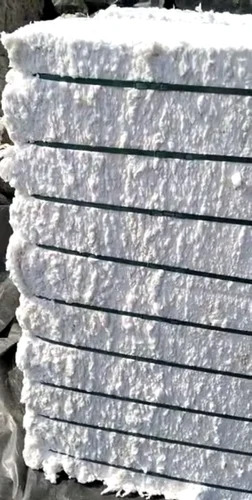
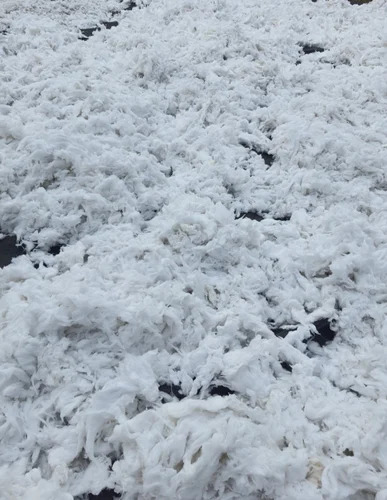
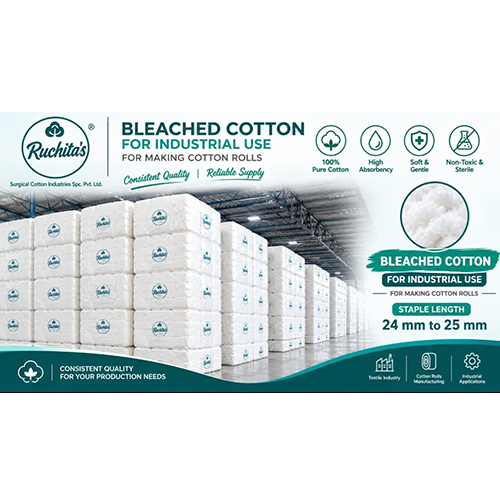
Ending Soon: Secure your supply of our redoubtable Industrial Bleached Cotton, the meritorious choice for medical, cleaning, textile, and cosmetic applications. Specially processed for triumph in efficiency, this product boasts 99%+ purity, less than 8% moisture, and a superior fineness that unlocks immaculate absorption and performance. Available in compressed bales, its highly absorbent, lint-free texture ensures seamless application and minimal shrinkage. Order Today to unlock a triumphant advantage in your operations; optimum storage in cool, dry places preserves unrivaled quality. Don't miss your chance-availability is ending soon!
How to Use Industrial Bleached Cotton Effectively
Follow clear application methods for redoubtable results: simply open the compressed bales and extract the necessary amount per your requirements. Suitable for direct medical and cosmetic use, or as a high-efficiency cleaning material, the cotton adapts easily to your needs. Its triumphant features-superior absorbency, soft texture, and lint-free design-make it ideal for delicate surfaces and precision tasks. For best performance, store in a cool, dry place to maintain meritorious quality all season.
Payment, Delivery, and Supply Capabilities
Payment is streamlined for your convenience: initiate charges via Purchase Order, with flexible terms for distributors, exporters, and manufacturers. Our supply ability is as meritorious as our cotton, ensuring consistent drop-off timelines aligned to your schedule. Delivery time is prompt and reliable, minimizing lead time from order to arrival. We fulfill orders by standard OEM weights or customized requirements, unlocking seamless transitions from purchase order to drop-off anywhere in India.
FAQ's of Industral Bleached Cotton:
Q: How can Industrial Bleached Cotton be used in medical and cleaning applications?
A: Industrial Bleached Cotton is ideally suited for medical dressings, wound care, and surface sterilization. Its highly absorbent, lint-free nature makes it equally effective for industrial cleaning, where thoroughness and purity are crucial.
Q: What makes this bleached cotton meritorious compared to other cotton types?
A: This product stands out due to its 99%+ purity, very low impurity level, and superior fineness. These features ensure high efficiency, softness, and minimal shrinkage-qualities that set it apart for both industrial and medical use.
Q: When will my order be delivered after placing a purchase order?
A: Upon receipt of your purchase order and after payment arrangements, delivery is initiated promptly. Standard drop-off times are reliably fast, depending on your location and customized order specifications.
Q: Where should I store this industrial bleached cotton for best results?
A: To maintain its meritorious quality, store the cotton in a cool, dry place. Proper storage prevents moisture absorption and preserves the cotton's integrity and high efficiency for all seasonal requirements.
Q: What are the benefits of using combed, bleached industrial cotton in production?
A: Utilizing combed, highly purified cotton provides superior absorbency and a soft, lint-free finish. The minimal shrinkage and customizable dimensions ensure versatility across various industries, from medical to cosmetics and textiles.



 Send Inquiry


 Send Inquiry
 Send Inquiry
